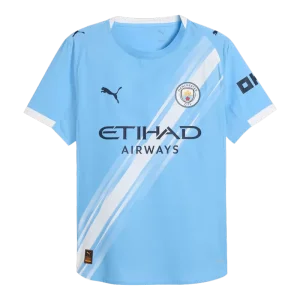
Explore our flagship high-demand football apparel collection, manufactured with precision textile engineering and international export compliance.
Understanding search intent, B2B procurement dynamics, and technical manufacturing requirements for high-margin sportswear distribution.
In modern digital trade, queries for a Best Man City Jersey Supplier & Suppliers represent high-intent commercial procurement. Global sports apparel buyers, retail chains, fan club outfitters, and e-commerce brand owners require transparent manufacturing capabilities, reliable fabric engineering, and seamless logistical execution. As Manchester City continues its global dominance across the English Premier League and UEFA Champions League, global retail demand for the iconic sky-blue kit has surged exponentially.
Meeting this intent requires more than standard apparel production. Distributors demand institutional-grade transparency regarding fabric GSM weight, color fastness ratings under FIFA-standard washing cycles, custom silicone heat-transfer applications, and strict compliance with international labor standards.
This technical whitepaper consolidates over a decade of OEM/ODM manufacturing expertise from BESTPOOL(BSP) Technology Co., Ltd. To ensure maximum Search Quality standards under Google's E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) framework, this guide provides empirical data on polyester micro-fiber mesh construction, zero-defect quality control protocols, and real-world supply chain contingency planning.
"Procurement managers do not just buy jerseys; they invest in supply chain stability, color precision matching (Pantone 292C Sky Blue), and localized import compliance."
Integrating state-of-the-art textile technology with scalable mass production in Guangzhou.
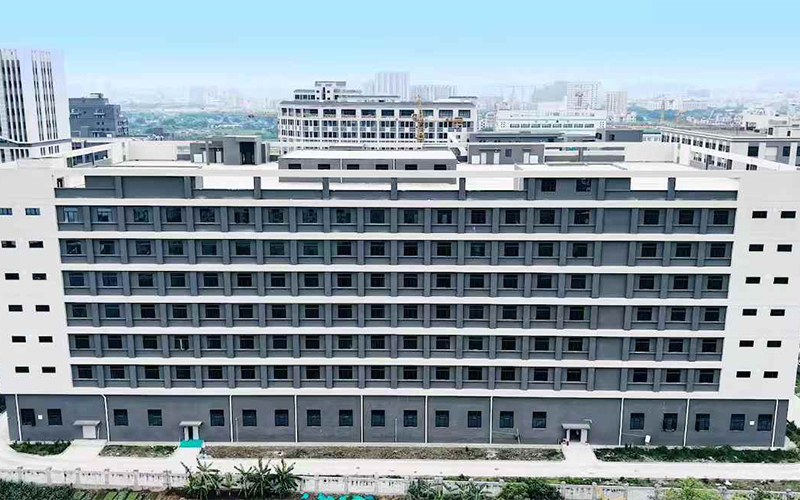
BESTPOOL(BSP) Technology Co., Ltd. is a premier professional supplier and factory manufacturer of high-grade soccer jerseys, basketball jerseys, activewear, and athletic accessories. With centralized manufacturing hubs located in Guangzhou and satellite production facilities in key textile provinces across China, we have refined our operational expertise since 2010.
We strictly adhere to the operational principles of "Quality First, Service First, Continuous Improvement, and Innovation to Meet Customer Needs." Our zero-defect management architecture targets "Zero Defects and Zero Complaints" across every export shipping container leaving our facilities.
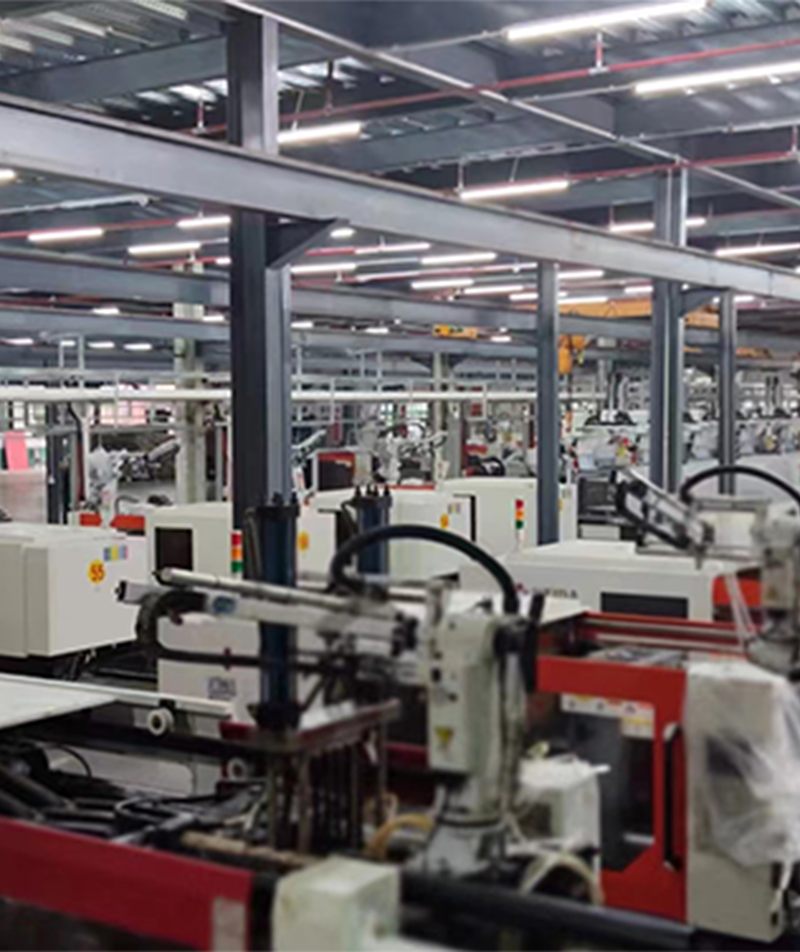
Our annualized factory output surpasses 1,000,000 finished garment pieces. By scaling high-efficiency laser cutting lines, automatic sublimation printers, and computerized stitching tables, we deliver rapid turnover rates for both bulk catalog stock and tailored custom OEM orders.


Breakdown of textile specifications, breathability matrix, badge pressing, and durability engineering.
Utilizing 150-180 GSM high-gauge recycled polyester micro-fibers. Features open-cell Jacquard structure for optimal breathability and body temperature control during high-intensity matches.
Italian Kian™ eco-friendly digital sublimation inks guarantee precise Pantone Sky Blue matching. Hydrophobic fixation processes eliminate color bleeding and fading across 100+ industrial wash cycles.
Supplying both embroidered silicone crests and high-definition ultra-thin hot-melt TPU badges for authentic player-version kits, minimizing friction against athlete skin.
Flatlock four-needle six-thread seam construction reduces tensile stress under continuous dynamic strain, preventing seam bursting and boosting garment longevity.
Navigating global supply chain volatility, inventory turning speeds, and international trade channels.
The worldwide sportswear market is undergoing a seismic shift toward flexible, low-lead-time supply chains. For distributors targeting Man City merchandise and contemporary European club uniforms, relying on rigid, multi-month production schedules is no longer viable. Bestpool Technology provides rapid agility for global buyers, operating streamlined production lines that seamlessly switch between stock replenishments and custom OEM modifications.
By leveraging China's robust raw material ecosystem in Guangdong, we maintain strategic safety buffers for high-demand yarns, knitted collar ribbing, and zip fasteners. This infrastructure insulates global clients against raw material shortages during peak tournament seasons.
Our export pipeline spans over 45 countries across major sports markets. We provide tailored pricing tiers, transparent freight forwarding protocols (FOB Guangzhou, CIF, DDP), and standardized batch labeling to meet diverse regional requirements.
Mitigating cross-border trade risks through stringent testing standards and localized regional logistics support.
All textiles meet OEKO-TEX Standard 100 environmental criteria, confirming zero hazardous chemical substances, AZO dyes, or heavy metals—guaranteeing full safety compliance for European and North American markets.
We provide full-service Customs Clearance and Freight Forwarding (DDP/DDU) for major regional hubs across North America, Europe, Latin America, and Southeast Asia, streamlining import procedures for seamless delivery.
Products arrive fully retail-ready with standardized hangtags, custom polybags, universal UPC/EAN barcode labels, and size stickers configured for immediate distribution upon delivery.
Tailored supply chain solutions engineered for diverse commercial monetization models.
Turnkey inventory distribution designed for high-turnover online stores, Amazon sellers, and regional retail storefronts seeking dependable restocking cycles and competitive unit margins.
Bulk customization tailored for global supporter organizations, incorporating custom sleeve patches, commemorative chest text, and personalized player name/number thermal vinyl applications.
Durable, high-tensile athletic kits engineered to withstand rigorous training routines, high-frequency laundering, and dynamic turf abrasion for youth soccer programs.
Co-branded apparel packages integrating corporate logo placements alongside classic club designs for high-impact promotional giveaways, corporate tournaments, and experiential marketing campaigns.
Complementary high-volume football kit lines manufactured with identical precision, material integrity, and quality control.
Innovating next-generation smart textiles, eco-friendly fabric technologies, and automated supply chains.
Transitioning our complete jersey line to ocean-bound ocean plastics and post-consumer recycled rPET yarns, lowering carbon emissions by 40% per garment produced.
Integrating phase-change materials (PCM) into professional authentic player kits to continuously regulate micro-climate skin temperatures during extreme heat conditions.
Deploying AI-driven automated cutting and print systems to reduce custom sample prototyping times from 7 days down to 24 hours.
Direct answers regarding minimum order quantities, customization workflows, freight logistics, and fabric guarantees.
A: For catalog stock items, our flexible MOQ starts at just 10-50 pieces per design. For fully customized OEM orders featuring unique sponsor logos or localized sizing tags, the MOQ typically begins at 100 pieces per batch.
A: We utilize advanced Spectrophotometer digital color matching system coupled with imported Italian sublimation inks. Physical lab dips and digital color proofs are submitted for written buyer approval prior to starting bulk production.
A: Yes, all fabrics produced by BESTPOOL(BSP) Technology Co., Ltd. comply with OEKO-TEX Standard 100, REACH regulations, and BSCI factory audit standards, ensuring complete safety for export into EU, US, and Asian markets.
A: Absolutely. Our factory floor houses multi-station automated pneumatic heat-press machinery using anti-sublimation block-out transfer vinyl to prevent dye migration into personalized names and numbers.
A: Sample prototypes are typically dispatched within 3 to 5 business days. Mass production orders require 12 to 18 days depending on total order volume. Express air freight (DHL/FedEx/UPS) takes 3-5 days, while ocean shipping spans 20-30 days.
A: We maintain a 4-tier inspection workflow: Raw Fabric Inspection (AQL 1.5 standard), In-line Sewing Checks, Post-Sublimation Color Verification, and Pre-Packing Final Audits to maintain our 99.8% pass rate goal.
Expand your catalog with our top-selling football kits engineered for peak retail turnover.
 BESTPOOL