The international sportswear procurement landscape has undergone a tectonic shift toward high-velocity supply chains, intelligent material engineering, and ultra-rigorous compliance standards. As sports merchandising evolves into an omnipresent lifestyle category, global demand for Manchester United-inspired t-shirts, fanwear apparel, and performance match kits has reached unprecedented commercial volumes. Sourcing directors, independent retail chains, e-commerce brand builders, and regional distributors require manufacturing partners who offer more than basic cut-and-sew services. They demand full-spectrum OEM/ODM integration, intelligent fabric R&D, eco-certified raw materials, and seamless customs clearance protocols.
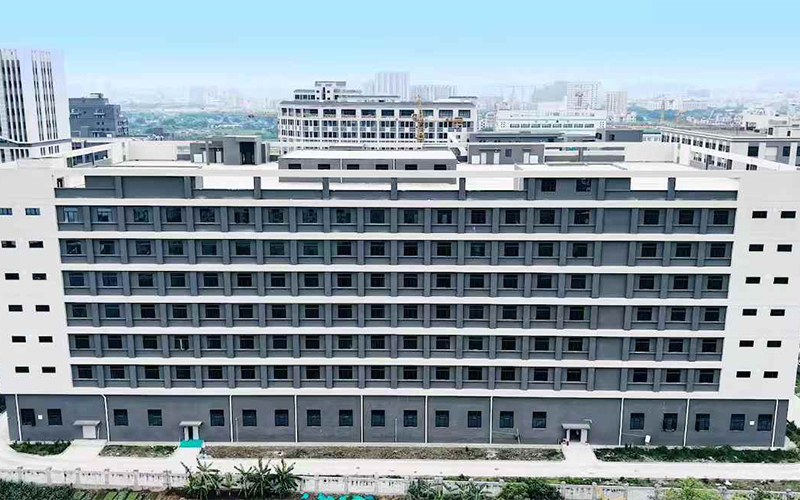
BESTPOOL (BSP) Technology Co., Ltd. operates at the nexus of technical innovation and scalable manufacturing. Established in 2010 with expansive production hubs centered in Guangzhou, South China’s premier textile epicenter, BSP provides turnkey commercial manufacturing solutions. With an annual capacity exceeding 1,000,000 finished garments, our facility bridges the critical gap between high-volume bulk efficiency and micro-detail craftsmanship, ensuring zero defects across complex sportswear production runs.
When enterprise purchasers evaluate a Wholesale Man Utd Tshirt Manufacturer & Factories, their semantic search criteria encompass a multi-faceted matrix of technical parameters. Modern intent mining reveals that commercial procurement decisions hinge on five foundational pillars:
BESTPOOL(BSP) Technology Co., Ltd. is a premier international supplier and specialized manufacturer of high-grade soccer jerseys, basketball kits, sportswear shorts, club replica uniforms, national team gear, and custom athletic training jackets. Founded in 2010, our company has cultivated a centralized operational infrastructure headquartered in Guangzhou, leveraging direct access to world-class supply chains for technical textiles, specialized trims, and dye sublimation inks.
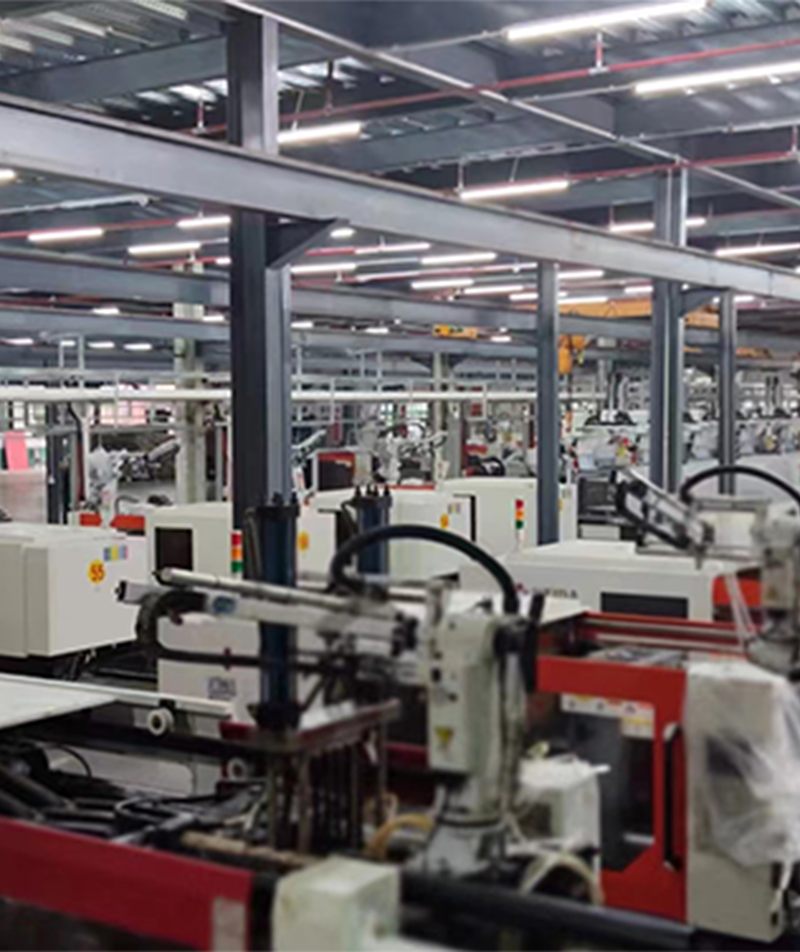
Our expansive manufacturing network integrates computerized pattern-making, automated laser cutting tables, multi-head high-speed embroidery systems, and continuous-feed rotary heat transfer machinery. In a short period of time, we have systematically expanded our production capacity to seamlessly satisfy rising foreign market demands across Europe, North America, Latin America, Southeast Asia, and beyond.
Football is more than a sport — it's a global way of life and an economic powerhouse. At BSP, we engineer sports apparel that reflects this passion through uncompromising technical excellence. Our core activities include:
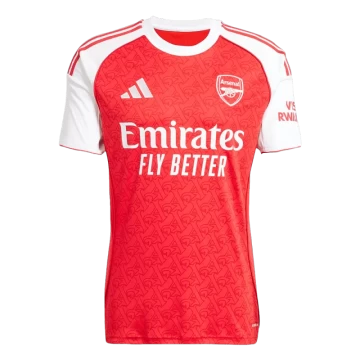
Arsenal Edition
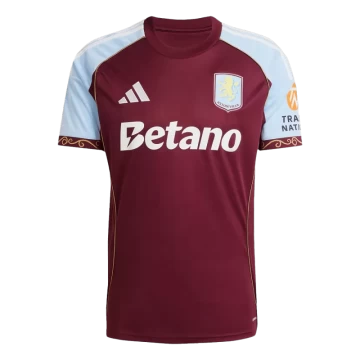
Aston Villa Edition
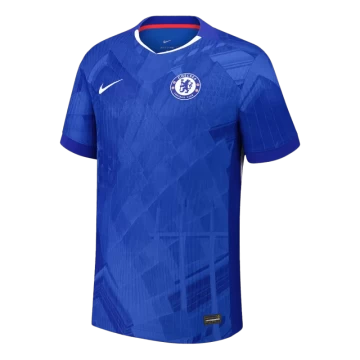
Chelsea Edition
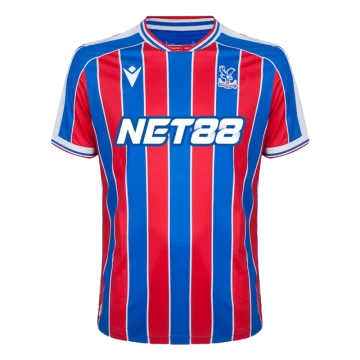
Crystal Palace Edition
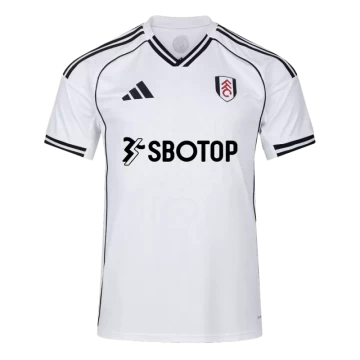
Fulham FC Edition
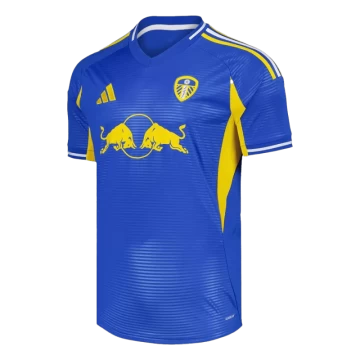
Leeds United Edition
Our Man Utd style performance tees incorporate 3D engineered polyester structures featuring specialized cross-section yarns. These hydrophilic fibers pull moisture away from the skin through capillary action, accelerating sweat evaporation and keeping athletes cool under high-intensity physical exertion.
We provide versatile embellishment options for wholesale clients, including woven high-density badges, heat-applied TPU 3D crests, raised rubber silicon prints, and ultra-crisp direct-to-film (DTF) logo integrations built to withstand rigorous washing protocols.
Aligning with global decarbonization mandates, our manufacturing lines offer 100% Recycled Polyethylene Terephthalate (rPET) fabrics derived from post-consumer plastic bottles. All sublimated prints utilize REACH-compliant, non-toxic water-based inks.
Execution excellence at BESTPOOL Technology is governed by an automated, four-stage manufacturing roadmap designed for absolute quality control:
Digital pattern grading, vector artwork adjustments, Pantone color matching, and 3D digital garment prototyping.
High-temperature (210°C) digital sublimation printing onto raw rolls, ensuring vivid, deep fiber saturation.
Precision laser cutting followed by 4-needle 6-thread flatlock stitching for maximum seam durability and friction reduction.
AQL 1.5 standard multi-point inspection, needle detection screening, individual polybagging, and anti-counterfeiting tag attachment.
If you are interested in our company or factory, please feel free to send us an email for negotiation at any time, and you are also welcome to come for on-site inspection. We will provide you with the best service with the utmost sincerity.
We mainly export our products to Europe, America, Mexico, South America, South Africa, East South Asia, Japan, Korea, etc. Our goal is to reach the expectations of sports fans, bringing you the latest and greatest sportswear with an affordable price, faster delivery and safer shopping!


To provide an extensive range of high quality goods at the most competitive factory direct prices.
To work alongside our valued customers to develop their businesses incrementally.
To maximize the profitability, competitiveness and sustainability of our international buyers.
To strategically utilize market trends and business intelligence to serve our customers’ diverse sourcing and procurement needs.
Our manufacturing operations fully comply with major global import and safety standards, including EU REACH chemicals regulations, US CPSIA safety guidelines, and UK C-TPAT supply chain security norms, ensuring zero customs holds for bulk shipments.
We support custom multi-currency retail hangtags, localized language packaging, EAN/UPC barcode printing, and Amazon FBA warehouse-ready prep including custom inner carton distribution setups.
Leveraging direct contracts with DHL, FedEx, UPS, and ocean freight shipping alliances, we provide FOB Guangzhou/Shenzhen, CIF, and DDP (Delivered Duty Paid) door-to-door logistics services globally.
For custom OEM/ODM production runs requiring tailored dyeing or custom fabric weights, our standard MOQ is 50 to 100 pieces per design/colorway. For existing stock jersey blanks and standard color sublimations, we support micro-wholesale orders starting as low as 10 to 20 pieces, enabling retailers to test regional market demand without excess capital tie-up.
We utilize computerized Pantone Matching System (PMS) technology paired with spectrophotometer color analysis. Our sublimation hardware operates with original Japanese printheads and premium Italian ink formulations, guaranteeing crisp line definitions, vibrant true reds, and zero color shifts across repeat bulk orders.
Sample creation and pre-production proofing take 3 to 5 business days. Once samples are confirmed, mass production of 1,000 to 10,000 units is typically completed within 15 to 20 days. Air express delivery (DHL/FedEx) requires an additional 4 to 7 days, while ocean or rail freight takes 20 to 35 days depending on the destination port.
Yes, absolutely. We provide complete turnkey white-label and private-label packaging solutions. This includes woven neck labels, heat-transfer inner size prints, customized branded hangtags, holographic security seals, and printed zipper polybags formatted with client-specific barcodes and SKU data.
We execute a strict 4-stage inline inspection workflow: 1) Incoming fabric raw material testing for weight, elasticity, and colorfastness; 2) Post-printing visual alignment checks; 3) Mid-assembly seam-strength inspection; and 4) Final AQL 1.5 garment audit including thread trimming, iron pressing, and metal needle detection.
 BESTPOOL