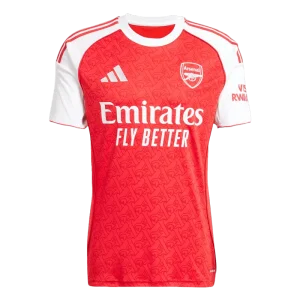
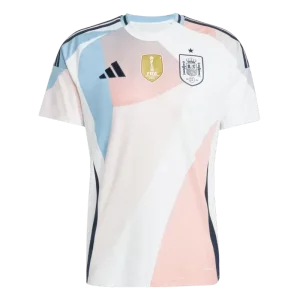
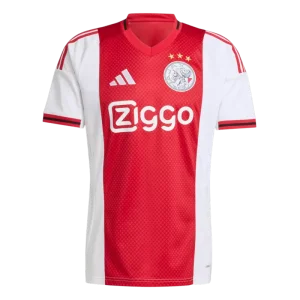
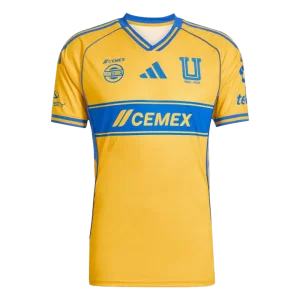
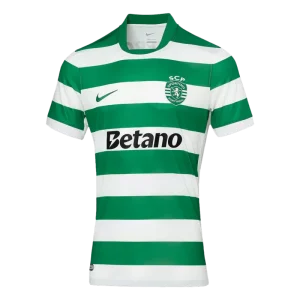
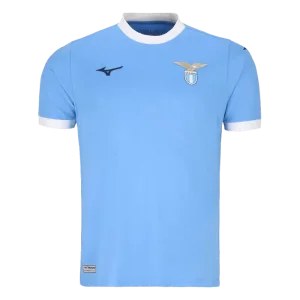
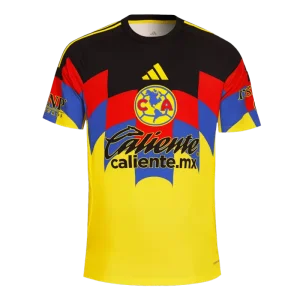
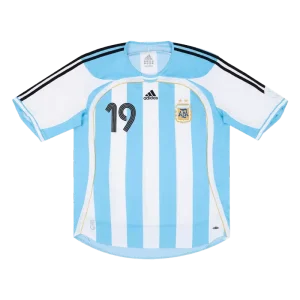
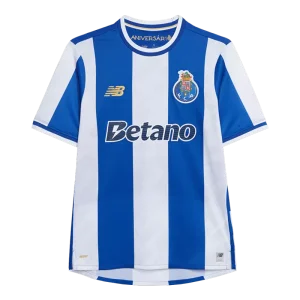
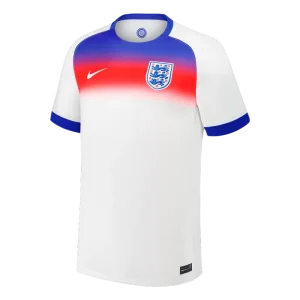
High-demand commercial designs engineered with premium micro-mesh fabrics and high-precision sublimation printing for international distributors.
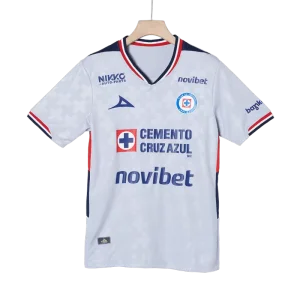
An exhaustive analysis of market capitalization, fan demographic evolution, retail demand shifts, and wholesale supply chain mechanics across global territories.
The global market for professional football merchandise, particularly iconic club apparel such as red Liverpool-style soccer jerseys, has evolved from localized fan purchasing into a multi-billion-dollar international asset class. Driven by the expansion of top-flight European leagues into Asia-Pacific, North America, and Latin American territories, the demand for high-grade OEM and ODM bulk apparel manufacturing has reached unprecedented heights. Sourcing directors, independent retail chain buyers, and e-commerce brand owners face an increasingly sophisticated end-user base that demands true-to-pitch aesthetics, optimal durability, and high thermal performance.
To capture market share in this ultra-competitive environment, B2B procurement partners must move beyond basic garment assembly. Today's commercial success depends on securing supply chain relationships with tech-enabled manufacturers capable of rapidly scaling production while maintaining stringent batch consistency. The proliferation of digital sports broadcasting, social media fandom, and grassroots football academies has created a year-round purchasing ecosystem that transcends traditional match-day seasonal spikes.
Historically, global sportswear production was concentrated heavily in single-region hubs. However, modern supply chain risk mitigation strategy demands a hybrid industrial operational model. Modern manufacturing clusters in southern China, particularly around the Guangzhou industrial corridor, combine advanced textile research institutions with automated cutting-edge assembly facilities. This enables unprecedented agility: converting concept tech-packs into commercial production runs in as few as 14 business days.
By leveraging integrated industrial clusters, primary suppliers can source raw micro-denier yarns, custom dye formulations, and eco-certified recycled polymers with zero lead-time latency. This micro-ecosystem allows global wholesalers to lower holding costs, mitigate overstocking risks through flexible minimum order quantities (MOQs), and pivot swiftly to emerging micro-trends within international sportswear markets.
Deconstructing the physical properties, moisture-management vectors, and yarn constructions required for professional-grade performance jerseys.
Modern athletic performance hinges on capillary action engineering. High-tier Liverpool-style jerseys utilize dual-knit micro-polyester structures featuring hydrophobic inner layers and hydrophilic outer matrices. Moisture is immediately pulled away from the athlete's skin through capillary force, spreading over an expanded surface area on the outer fabric face to accelerate evaporative cooling during intensive exertion.
Achieving the optimal ratio between lightweight comfort and tear resistance is paramount. Commercial fan-replica variants generally leverage 150 to 165 GSM interlock polyester, providing soft hand-feel and retail-ready drape. Player-issue specifications utilize ultra-lightweight 130 to 145 GSM jacquard micro-mesh featuring engineered ventilation zones without compromising burst strength under competitive physical stress.
In response to international environmental regulations such as the EU's Sustainable Textiles Directive, premier factories utilize 100% rPET (recycled Polyethylene Terephthalate) yarns derived from post-consumer plastic bottles. These recycled fibers undergo rigorous depolymerization and spinning processes to match the tensile strength, color clarity, and soft touch of virgin synthetic polymers.
| Specification Metric | Fan Replica Standard | Match Authentic (Player Issue) | Testing Standard / Compliance |
|---|---|---|---|
| Fabric Composition | 100% Micro-Polyester Interlock | 92% rPET + 8% Elastane Jacquard Mesh | ISO 1833-1 Fiber Analysis |
| Fabric Weight (GSM) | 160 GSM ± 5g | 135 - 145 GSM ± 5g | ASTM D3776 Standard Grammage |
| Moisture Wicking Speed | < 3.0 Seconds Absorption | < 1.0 Second Immediate Wicking | AATCC 79 Absorbency Test |
| Color Fastness (Washing) | Grade 4.0 - 5.0 | Grade 4.5 - 5.0 | ISO 105-C06 Color Retention |
| Emblem Application | High-Density Direct Embroidery | 3D Heat-Transferred TPU / Silicone | ISO 6330 Wash Durability (50 Cycles) |
| Tensile Strength | > 350 N Longitudinal | > 420 N Reinforced Seam Construction | ASTM D5034 Grab Test |
From raw filament inspection to automated packaging: How certified factories achieve zero-defect operational outcomes.
Engineering begins with precision Computer-Aided Design (CAD) pattern creation tailored to regional sizing grids (EU, US, Asian fit). Automated nesting software optimizes fabric yield, reducing material waste below 3.5%.
Utilizing high-speed Italian printheads and eco-certified Swiss inks, custom graphics and vibrant club red shades are deeply infused into synthetic fibers at 210°C, preventing cracking, fading, or peeling over prolonged use.
Computer-controlled laser cutting tables trim printed fabric panels with sub-millimeter precision. Heat-sealed edges prevent fraying during subsequent stitching and enhance overall seam integrity.
Assembly line sewing machines utilize flatlock 4-needle 6-thread technology. This creates ultra-flat, non-chafing ergonomic seams capable of withstanding extreme mechanical pull forces on the pitch.
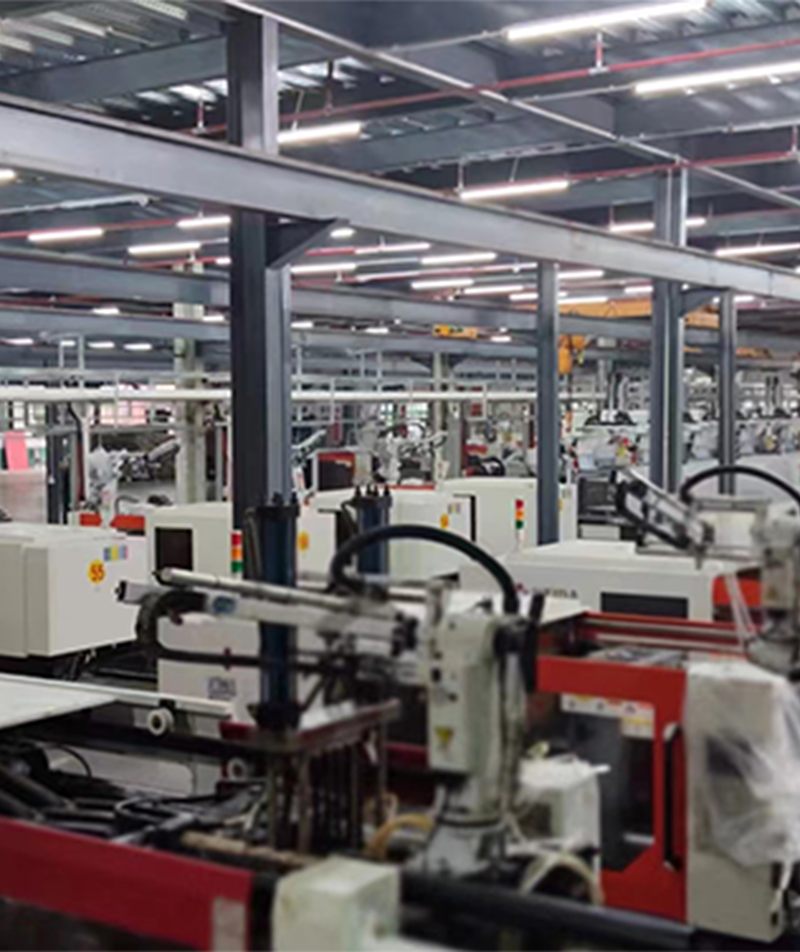
A premier OEM/ODM manufacturing enterprise dedicated to powering world-class athletic brands, wholesale importers, and teamwear distributors since 2010.
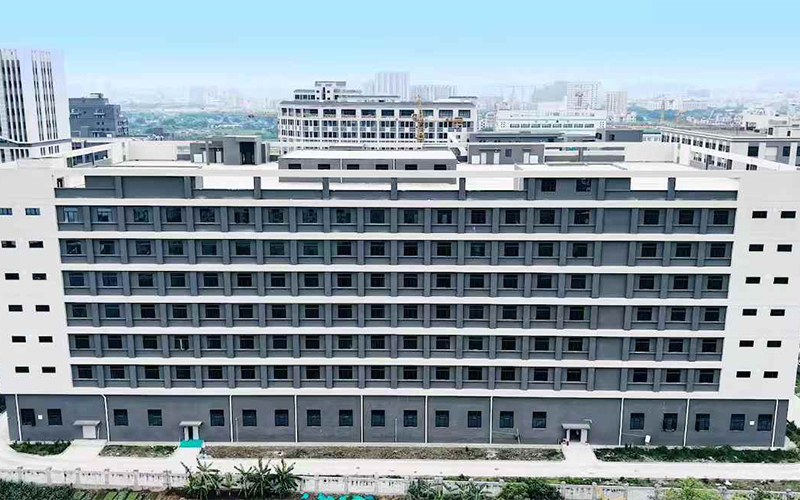
BESTPOOL (BSP) Technology Co., Ltd. is a professional supplier of soccer jerseys and basketball jerseys, with state-of-the-art manufacturing facilities strategically situated in Guangzhou and key industrial cities across Southern China.
With professional sales and manufacturing experience established in 2010, we strictly adhere to the fundamental management principle of "quality first, service first, continuous improvement and innovation to meet customer needs". Our non-negotiable benchmark is achieving "zero defects and zero complaints" across all production runs.
We supply the latest high-quality soccer jerseys, basketball jerseys, performance shorts, complete match kits, hot club jerseys, national team kits, and technical training jackets. With an annual capacity exceeding 1,000,000 pieces, we rapidly scale production to fulfill expanding global demand. We maintain robust technical capabilities, advanced R&D infrastructure, fast inquiry turnaround times, and comprehensive 24/7 client support. Football is more than a sport — it's a way of life.

Tailored supply chain strategies aligned with specific commercial channels across primary international sales regions.
Designed for fast-moving Amazon, Shopify, and eBay merchants. We maintain high safety-stock inventories of generic blank templates and top-selling colorways, enabling custom sleeve badge heat-pressing and dispatch within 48 hours to minimize delivery windows for international online shoppers.
Geared towards physical retail store networks across Europe, Latin America, and North America. We provide custom retail packaging, barcoding, hangtags, and point-of-sale display integration, backed by robust batch consistency and compliant country-of-origin documentation.
Serving amateur leagues and educational institutions requiring bespoke squad kits. Our flexible customization workflow supports individual player numbering, local sponsor logo screen printing, and embroidered club crests with minimum order quantities as low as 10 sets per style.
Integrating smart textiles, waterless dyeing innovations, and AI-driven supply chain forecasting into high-volume apparel manufacturing.
The next decade will blur the line between traditional sportswear and functional athletic technology. Future generations of Liverpool-style performance shirts will feature woven micro-conductive threads and ultra-thin NFC tags. These embedded components enable real-time tracking of biometric data for academy players, while providing retail consumers with instant digital authenticity verification via smartphone scanning.
Environmental stewardship requires radical manufacturing innovations. BESTPOOL is evaluating supercritical carbon dioxide (scCO2) dyeing equipment for future production expansion. This dry dyeing process eliminates liquid water usage entirely, reduces energy consumption by 45%, and eliminates chemical effluent discharge while achieving unmatched color depth in synthetic fibers.
Strategic frameworks for B2B buyers to navigate tariff shifts, sea-freight volatility, and inventory risk mitigation.
Navigating changing international import tariffs requires clear product classification. We assist international importers with accurate HS Code classifications (e.g., HS 6109.30 for synthetic T-shirts/jerseys), preferential trade origin certificates (Form A, RCEP), and compliant custom declarations to prevent customs holds and duty overpayment.
To shield clients from global shipping delays and freight rate spikes during peak holiday seasons, we offer Vendor-Managed Inventory (VMI) services. Core raw materials and unprinted body blanks are buffered in our Guangzhou warehouses, guaranteeing rapid manufacturing response during high-demand tournaments.
Our logstics team offers comprehensive DDP (Delivered Duty Paid), FOB, and CIF shipping options via express air freight (DHL, FedEx, UPS), ocean container transport (FCL/LCL), and cross-border rail connections directly to European distribution hubs.
Direct expert insights resolving commercial inquiries, technical fabric standards, and factory ordering procedures.
Fan Replica jerseys are engineered primarily for comfort, casual wear, and long-term laundering durability, using a slightly heavier 160 GSM interlock micro-polyester with traditional high-density woven or embroidered club crests. Player-Issue (Match Authentic) versions prioritize performance and weight reduction, using an ultra-lightweight 135–145 GSM jacquard ventilation fabric, athletic slim-fit tailoring, laser-cut ventilation ports, and heat-pressed 3D silicone/TPU lightweight crests.
We utilize the Pantone Matching System (PMS) along with spectrophotometric digital color testing. Our digital sublimation transfer process relies on premium Italian inks calibrated to hit exact Pantone targets (such as classic Crimson Red and Scarlet shades). Each production batch undergoes color fastness testing under ISO 105-C06 standards, guaranteeing a color retention grade of 4.5+ after 50 industrial wash cycles.
For fully customized ODM designs requiring custom yarn dyeing or unique knitting patterns, our standard MOQ is 500 pieces per design. However, for standard sublimated styles, stock-pattern customization, or team kit runs using our catalog blanks, we accommodate flexible MOQs starting at 10 to 50 pieces per order, supporting growing e-commerce brands and regional club suppliers.
Our partner factories maintain international certifications including ISO 9001 for Quality Management Systems, WRAP (Worldwide Responsible Accredited Production) for ethical labor conditions, and OEKO-TEX Standard 100 certification for raw fabric safety. This ensures our garments are free from harmful heavy metals, azo dyes, and phthalates.
Yes, we offer complete OEM private-label packaging solutions. This includes heat-transfer tagless neck labels, custom branded woven neck tapes, customized hangtags with scannable EAN/UPC barcodes, and 100% biodegradable or recyclable polybags designed for direct retail display.
Physical sample development typically takes 3 to 7 business days following digital CAD tech-pack approval. Once the pre-production sample is confirmed, bulk manufacturing cycles range between 12 to 21 business days, depending on overall volume and decoration complexity. Express air freight options allow door-to-door delivery within 5 to 7 days globally.
Explore our full line of club, national, and retro replica soccer jerseys manufactured to stringent export specs.
 BESTPOOL