Engineered for global wholesalers, sports retail chains, and official distributors. High GSM durability and elite athletic performance fit.
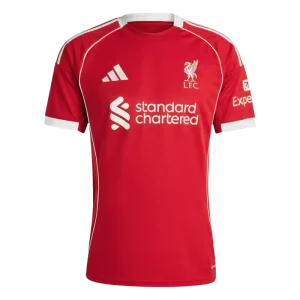
An in-depth operational framework analyzing textile yarn density, thermoregulation dynamics, OEM supply chain risk mitigation, and automated apparel manufacturing.
Navigating the international sportswear market requires a rigorous understanding of dynamic consumer expectations, brand equity compliance, and material engineering standards. When sourcing commercial volumes of Liverpool FC tops, authentic player-issue kits, and stadium replica shirts, global importers must balance cost structures with strict quality benchmarks.
Today's sport-retail landscape demands apparel that withstands rigorous physical exertion while retaining vibrant color integrity, structural elasticity, and tactile comfort. Modern supply chains no longer rely on simple stitch-and-sew sub-contracting; they demand integrated tech-driven ecosystems capable of handling custom dye sublimation, micro-ventilation mapping, and anti-counterfeiting serialization.
Procurement teams operating in North America, Europe, LATAM, and the Asia-Pacific region require transparent factory protocols. Key attributes such as Grams per Square Meter (GSM), yarn denier count, color fastness to perspiration, and seam tensile strength govern product longevity.
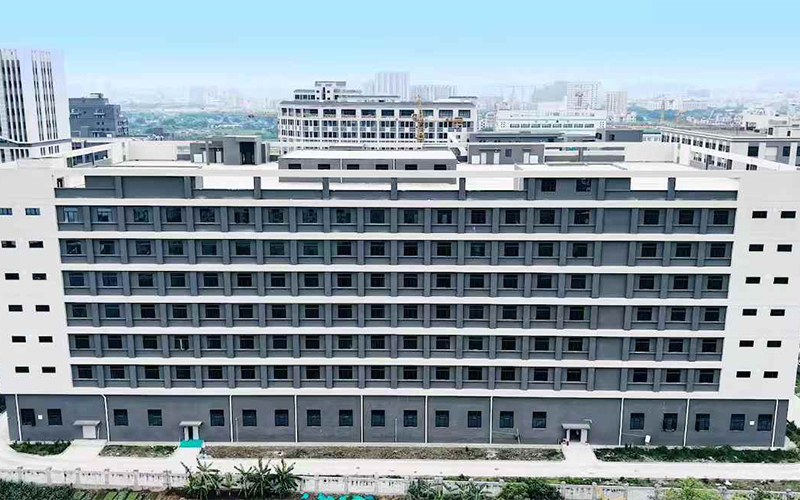
As a leading tier-1 sports garment manufacturer, our Guangzhou production hubs merge precision engineering with industrial agility. We enable brand owners, independent distributors, and fan-club outfitters to scale their wholesale operations without sacrificing technical compliance or margin viability.
Exploring advanced polymer chemistry, bio-based synthetics, and digitalized heat transfer systems for professional football tops.
Our next-generation Liverpool FC tops feature GRS-certified (Global Recycled Standard) rPET yarn extracted from ocean-bound plastics. Combined with 12% high-grade Spandex/Elastane, the fabric yields an extraordinary 4-way stretch matrix with immediate elastic recovery.
Utilizing body-mapping 3D knit techniques, key sweat zones (chest, spine, and underarms) feature micro-perforated channels. This engineered weave accelerates evaporative cooling, reducing fabric wet-weight by up to 34% during high-intensity matches.
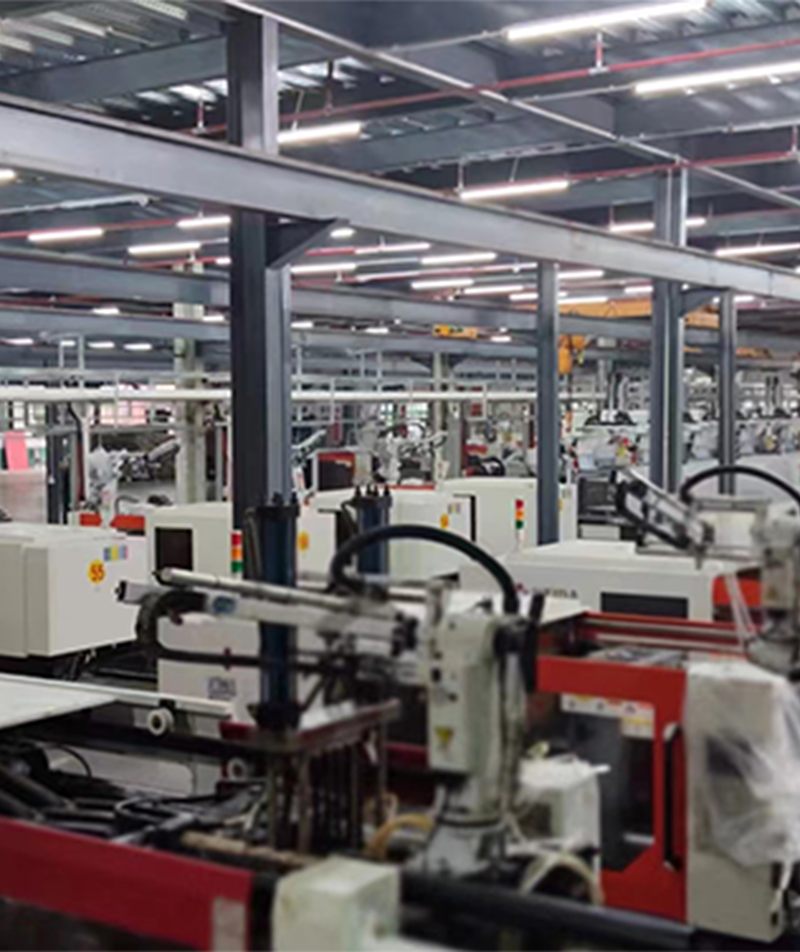
Moving beyond traditional flat embroidery, our factory utilizes automated high-frequency thermopress equipment to apply raised 3D TPU and flexible silicone club badges. This ensures zero internal skin friction while offering pristine visual dimension.
Technical Benchmark: Every wholesale unit produced in our facility undergoes 50+ industrial wash cycle tests at 40°C to guarantee zero peeling of heat-applied logos, sponsor prints, or player lettering.
How our automated Guangzhou manufacturing infrastructure mitigates lead-time volatility and ensures bulk delivery precision.
Precision begins at the cutting phase. By deploying computerized CAD pattern nesting alongside laser-guided automated cutting beds, we achieve pattern tolerance accuracy within ±0.5mm. This minimizes raw fabric wastage, optimizes cost efficiency, and ensures identical sizing across thousands of shirts.
Our Manufacturing Execution System (MES) digitally monitors every stage of your wholesale order—from greige fabric knitting and disperse dye application to final polybag sealing. Enterprise clients receive automated production status reports, ensuring complete visibility over transit schedules.
Tailored OEM/ODM manufacturing packages structured for regional importers, sports clubs, e-commerce giants, and retail networks.
We provide full-service private label conversion. Specify custom neck labels, woven hem tags, custom barcode hangtags, and branded eco-friendly polybags. Our design team converts flat vector graphics into production-ready tech packs within 24 hours.
Whether launching a targeted regional campaign or restocking large warehouse networks, our production lines accommodate flexible Minimum Order Quantities (MOQs) while offering tiered volume discounts for batch orders exceeding 10,000 units.
Protect brand integrity with optional woven security threads, custom optical holograms, and integrated RFID micro-chips directly embedded into jersey side seams for instant supply chain inventory scans.
Fulfilling global trade compliance, chemical safety standards, and environmental directives across international jurisdictions.
All fabrics, dyes, and heat-transfer films utilized in our Liverpool FC tops undergo stringent testing to meet OEKO-TEX Standard 100 and EU REACH regulations. They are certified completely free of hazardous azo dyes, heavy metals, formaldehyde, and perfluorinated chemicals (PFCs).
Our international trade desk assists global buyers with precise Harmonized System (HS) code classification (e.g., HS 6109.90 for synthetic knit tops), certificate of origin documentation (Form A, Form E), and Duty DDP/DAP freight forwarding options to streamline customs clearance.
Pioneering professional sportswear manufacturing and global distribution excellence since 2010.
BESTPOOL (BSP) Technology Co., Ltd. is a leading specialized manufacturer and exporter of football jerseys, basketball jerseys, and custom athletic wear. Operating state-of-the-art facilities in Guangzhou and surrounding industrial hubs, we maintain an annual output exceeding 1,000,000 finished pieces.
We operate under the core management framework: "Quality first, service first, continuous improvement and innovation to meet customer needs", targeting zero defects and zero complaints as our unyielding benchmark.
Corporate Motto: "Environmental protection as the purpose, efficient governance as the specialty, and energy saving as the goal. Heart to sunshine, everything to prosperity."


We produce premium quality replica and authentic kits across premier European leagues.
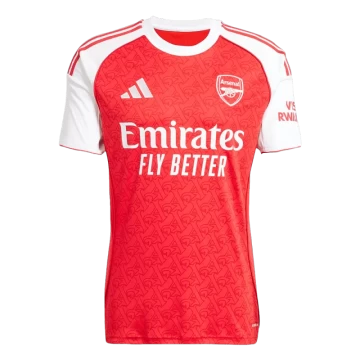
Arsenal Home Kit
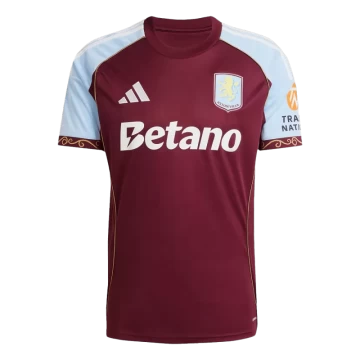
Aston Villa Home Kit
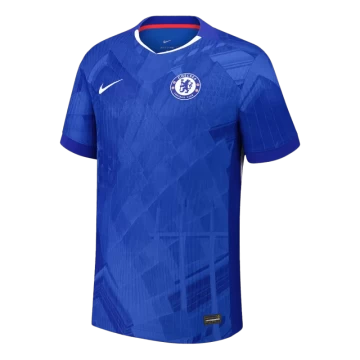
Chelsea Authentic Kit
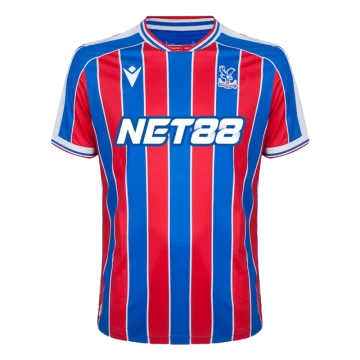
Crystal Palace Kit
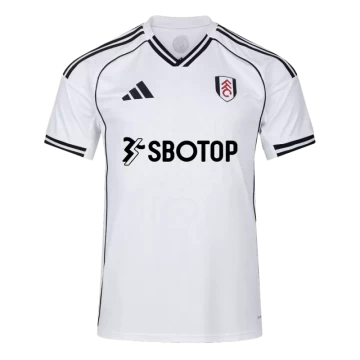
Fulham FC Kit
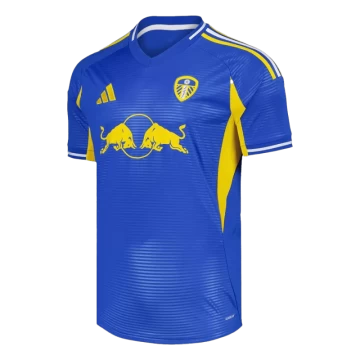
Leeds United Away
Addressing key operational inquiries regarding fabric specifications, customization protocols, shipping timelines, and compliance.
Authentic player-issue tops utilize an athletic slim fit, lightweight 140-150 GSM polyester-elastane micro-mesh fabric, heat-applied TPU rubberized crests, and targeted laser-cut ventilation holes designed for peak match performance. Replica tops feature a slightly looser standard fit, durable 160-180 GSM interlock fabric, and high-density embroidered badges suitable for everyday retail fan wear.
For ready-to-ship catalog stock, our MOQ starts at just 10-50 units per style. For fully customized OEM orders involving specialized dye sublimation colors, custom woven back-neck taping, and bespoke sleeve embroidery, our standard starting MOQ is 100 to 300 units per colorway.
We utilize X-Rite spectrophotometer color matching technology combined with digital Pantone Matching System (PMS) standards. Every dye lot is spectrophotometrically tested against master lab dips prior to full-scale knitting to ensure batch-to-batch color variance remains under Delta E < 1.0.
Pre-production physical samples are crafted and dispatched within 3-5 business days. Mass production generally requires 12-18 business days depending on total order volume. Air express shipping (DHL/FedEx/UPS) delivers within 4-7 days globally, while sea freight door-to-door options range from 20-35 days.
Yes. We offer fully customizable official-font vinyl heat-transfer printing for player names and numbers, along with official league sleeve badges (e.g., Champions League starballs, foundation badges, and league sleeve patches) using durable PU foil heat press systems.
Direct manufacturer pricing on national team and European club football shirts.
 BESTPOOL